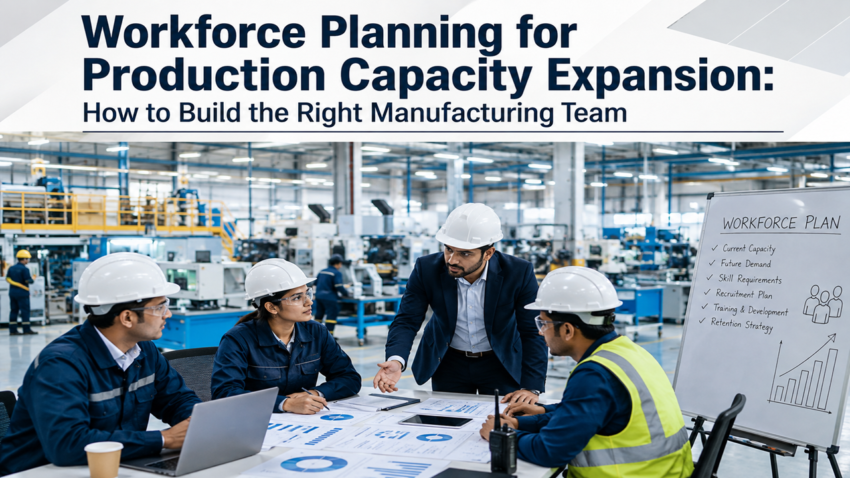
Increasing production capacity is not simply a matter of installing additional machinery or extending operating hours. A manufacturing plant must also have enough people with the right skills, availability and experience to support the higher production target.
For factory owners and plant managers, the challenge is determining whether the existing workforce can handle additional demand without increasing overtime, compromising product quality or creating operational delays.
A workforce that performs adequately at current production levels may struggle when output increases, particularly if certain operations depend on a small number of experienced employees.
Before approving additional recruitment or committing to a capacity expansion, manufacturers should evaluate workforce planning for factory expansion by assessing labour requirements, production bottlenecks, technical competencies and shift coverage together.
Why Existing Workforce Capacity Must Be Reviewed Before Expansion
A factory’s current workforce is usually organised around its existing production volume, equipment configuration and operating schedule. When any of these conditions change, the original staffing plan may no longer be sufficient.
For example, a manufacturer planning to increase daily output from 10,000 to 13,000 units might assume that hiring 30% more employees will solve the problem. However, this approach overlooks differences in machine capacity, product complexity, automation and work content.
Three situations commonly complicate workforce expansion:
-
Higher workload per shift: Existing employees may already be working near their practical limits, leaving little room for additional production.
-
New technical requirements: Additional machinery or automation may require competencies that the current team does not possess.
-
Uneven workload distribution: Some departments may have spare capacity while others become bottlenecks as production increases.
The objective is not necessarily to increase headcount. It is to establish whether the plant has sufficient productive hours and the necessary skills to achieve the proposed output reliably.
Establish the Actual Production Requirement
Before calculating manpower, define what the expansion must deliver.
Start by documenting the current production baseline and the proposed operating conditions.
Record the following information:
-
Current and target daily output.
-
Product mix and expected changes in production complexity.
-
Number of operating days per month.
-
Planned shifts and shift duration.
-
Current machine utilisation and downtime.
-
Quality rejection rates and rework requirements.
-
Expected date for reaching the new production target.
These details matter because an increase in finished units does not always translate into an equivalent increase in labour hours. A product redesign, automated process or change in batch size may alter the work required for each unit.
For example, a plant expanding production while introducing automated packaging may need additional maintenance and automation support, even if the number of packaging operators remains unchanged.
The assessment should therefore use the future production process rather than simply extrapolating from today’s employee count.
Calculate Manpower Requirements Using Actual Labour Content
One of the most useful starting points is calculating how much direct labour is required to produce the planned output.
The basic formula is:
Required operator-shifts = Total daily labour minutes required ÷ Productive minutes available per operator-shift
Daily labour minutes can be estimated by multiplying the target output by the standard labour content per unit.
Consider a hypothetical manufacturing plant with these operating conditions:
| Parameter | Current operation | Expanded operation |
|---|---|---|
| Daily production | 10,000 units | 13,000 units |
| Labour content per unit | 4 minutes | 4 minutes |
| Productive time per operator-shift | 420 minutes | 420 minutes |
| Required operator-shifts | 95.24 | 123.81 |
The calculations are:
-
Current requirement: 10,000 × 4 ÷ 420 = 95.24 operator-shifts.
-
Expanded requirement: 13,000 × 4 ÷ 420 = 123.81 operator-shifts.
-
Additional requirement: approximately 28.57 operator-shifts per production day.
Under these assumptions, the plant needs approximately 29 additional operator-shifts daily if labour content remains unchanged.
However, operator-shifts are not the same as individual employees. The final headcount depends on shift arrangements, weekly offs, leave, attendance, relief coverage and the distribution of required skills.
This calculation also assumes that four minutes represents the correct labour content per unit. If that figure is inaccurate or includes activities already accounted for elsewhere, the resulting estimate will be misleading.
For more reliable planning, validate standard work times using actual production observations and distinguish manual labour time from machine processing time.
Identify Production Bottlenecks Before Hiring
Aggregate manpower calculations provide an initial estimate, but they do not reveal where additional capacity is actually needed.
A factory may have sufficient employees overall and still fail to increase output because one operation cannot keep pace with the rest of the production line.
For example, consider a line targeting a 45-second cycle time per unit.
| Workstation | Actual cycle time | Assessment |
|---|---|---|
| Component preparation | 35 seconds | Potential spare capacity |
| Assembly | 55 seconds | Potential bottleneck |
| Final inspection | 40 seconds | Below target cycle time |
Assembly exceeds the target cycle time by 10 seconds. Adding employees to component preparation may not improve finished output if assembly remains the limiting operation.
Investigate the bottleneck before deciding whether to recruit.
Useful questions include:
-
Is the operation short of trained operators?
-
Are employees waiting for materials or equipment?
-
Are changeovers consuming excessive production time?
-
Does the process require manual work that could be redistributed?
-
Is machine downtime restricting output?
-
Could improved fixtures, work methods or line balancing increase throughput?
Lean manufacturing guidance on standardized work emphasises work sequence, takt time and process capacity as tools for understanding how operations should be balanced.
Hiring is appropriate when a genuine labour constraint exists. If the constraint is equipment availability, poor process design or material flow, additional recruitment alone may increase costs without delivering the expected production improvement.
Assess Technical Skills and Critical-Role Coverage
Headcount does not show whether the workforce can perform the tasks required by an expanded operation.
A plant might have enough maintenance employees in total but lack technicians qualified to troubleshoot a new automated line. Similarly, existing operators may be experienced with current machinery but unfamiliar with revised process controls.
Create a role-based skills matrix covering:
-
Production and machine operation.
-
Mechanical and electrical maintenance.
-
PLCs, automation and instrumentation, where applicable.
-
Quality inspection and testing.
-
Process engineering and troubleshooting.
-
Shift supervision and production coordination.
For each role, record the required competency level, the number of competent employees, their shift allocation and the availability of backup personnel.
A practical assessment can use four levels:
-
Requires training.
-
Can perform tasks under supervision.
-
Can perform tasks independently.
-
Can troubleshoot problems and train others.
These are suggested assessment categories rather than universal industry standards.
Pay particular attention to roles where only one or two employees can perform a critical task. Such dependencies may become more serious when production expands or additional shifts are introduced.
The result should identify whether each gap requires recruitment, cross-training, reassignment or specialist support.
Verify Shift Coverage and Realistic Employee Availability
An employee count is meaningful only when it reflects the hours and shifts during which people are actually available.
Suppose a plant has 60 operators. That number does not establish whether it can staff two production shifts adequately, because the calculation must account for shift allocation, weekly rest days, planned leave, absenteeism and required skill coverage.
Start with a shift-wise roster and determine:
-
How many operators are required for each shift?
-
Which positions must remain covered throughout production?
-
How many qualified employees are available for each critical task?
-
Can trained employees provide relief during absences?
-
Will additional shifts create a shortage of experienced supervisors or maintenance technicians?
Avoid treating every scheduled working minute as productive time. Breaks, meetings, routine checks and other necessary activities must be reflected consistently in the available-time assumptions.
The U.S. Bureau of Labor Statistics explains labour productivity in terms of output relative to hours worked. This provides a useful foundation for comparing changes in production with changes in labour input.
For expansion planning, track both the total labour hours available and the distribution of those hours across required skills and shifts.
Decide Whether to Retrain, Redeploy or Recruit
Once the labour and competency gaps are identified, compare the available responses rather than assuming that every shortfall requires recruitment.
Redeploy existing employees when some departments have spare capacity and employees can safely perform the required work after any necessary training.
Retrain or cross-train employees when existing staff have a suitable foundation but lack specific machine, process or troubleshooting competencies. Include training time, supervised practice and competency verification in the expansion schedule.
Recruit additional employees when the required labour hours are unavailable, internal training cannot close a critical skill gap in time, or new shifts need additional coverage.
Use project-based technical specialists when the requirement is temporary, such as equipment installation, commissioning, automation integration or specialised troubleshooting.
Compare these options using total operational cost, not salary alone. Recruitment expenses, training, overtime, production disruption and the cost of inadequate technical coverage may all affect the decision.
Capacity requirements planning should also consider whether people, equipment and other production resources will be available when needed. CIPS provides further context on coordinating these requirements.
Validate the Workforce Plan Before Expanding Production
A workforce calculation is a planning estimate, not proof that the factory is ready for higher output.
Before finalising the staffing budget, validate the assumptions through production trials, shift-level workload reviews and practical competency assessments.
A useful readiness checklist includes:
-
Future production volumes and product mix are confirmed.
-
Actual labour content has been measured.
-
Equipment and process bottlenecks have been assessed.
-
Required staffing is documented by department and shift.
-
Critical technical skills and backup coverage are verified.
-
Recruitment and training lead times fit the expansion schedule.
-
Overtime and staffing costs have been compared.
-
Trial production and workforce readiness checks are planned.
Where possible, test the proposed operating model on a representative production run. Record output, downtime, quality performance, overtime and staffing gaps.
If actual performance differs from the plan, investigate the cause before committing to permanent additional headcount. The problem may require more people, a different skill mix, improved work methods or additional equipment.
How IMARC Engineering Can Help
IMARC Engineering can support manufacturers in assessing workforce requirements before a planned capacity expansion. Its Workforce Planning and Technical Staffing service can be relevant when businesses need to identify staffing gaps, evaluate technical skill requirements, plan workforce deployment or source specialised personnel for project execution. By connecting manpower planning with production and project requirements, manufacturers can make more informed decisions about recruitment, training and technical staffing before increasing capacity. The appropriate scope depends on the plant’s operational requirements and project timeline.
Speak With An Expert: https://www.imarcengineering.com/contact?service=workforce-planning-and-technical-staffing
Conclusion
Determining whether an existing workforce can support factory capacity expansion requires more than comparing current and future employee counts. Manufacturers must evaluate labour hours, process bottlenecks, technical competencies and shift coverage against the proposed production target. By validating these factors before investing in additional manpower, factory owners can make better-informed decisions, reduce avoidable staffing costs and prepare their operations for sustainable growth. The objective is to build a workforce that can reliably support the expanded production process.
Contact Us:
IMARC Engineering
Phone: +91-120-433-0800
Email: sales@imarcengineering.com
India: C-130, Sector 2, Noida, Uttar Pradesh 201301
LinkedIn: https://www.linkedin.com/showcase/imarc-engineering/