In a busy production floor where cocoa dust hangs in the air and fine medicinal powders behave almost like smoke, even a small mistake can turn into a costly problem. A supervisor watches a line of workers carefully filling pouches by hand, but the scene is far from calm. One slight tilt of a scoop, a bit of powder sticking to a glove, or a brief pause in attention is enough to create uneven weights and wasted product. Over time, these small inconsistencies start affecting output, packaging quality, and customer trust.
As demand grows and orders increase, the pressure on manual filling becomes harder to manage. This is where controlled automation begins to change the rhythm of the entire line, turning a fragile process into something far more steady and repeatable.
- Helps reduce product loss caused by spills and overfilling
- Keeps each pack closer to the intended weight for better consistency
- Maintains cleaner handling conditions by limiting direct contact
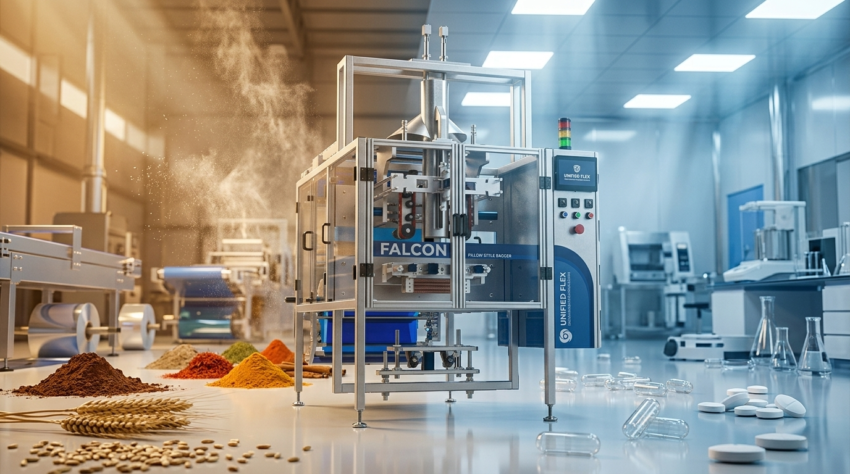
An automatic powder filling machine takes over this delicate stage by moving product through a closed system from hopper to container. Using controlled auger movement and measured vibration, it delivers steady fills even when powder density shifts during production. What used to depend heavily on operator skill becomes a repeatable process, helping manufacturers keep quality stable even during long production runs and high demand periods.
In powder production, precision is not just a measurement, it is the quiet force that decides product quality, consistency, and the trust a customer places in every sealed pack.
Challenges of Handling Fine Particles in Large Quantities
Working with powders presents unique physical challenges that differ greatly from liquids or solid goods. Fine particles can be prone to “bridging,” where they get stuck in the neck of a hopper, or “rat holing,” where only a small channel of powder flows through the center while the rest stays stuck to the sides. Automated systems are designed with internal agitators and vibratory bases that keep the material in a fluid state, allowing for a steady and predictable flow. Additionally, the dusting created by fine particles can be a health risk for workers and a maintenance nightmare for machinery if it is not contained. Modern equipment uses enclosed pathways and vacuum systems to catch stray dust before it can escape into the facility. These technical solutions ensure that the powder is handled with care, maintaining its texture and preventing the clumping that often occurs during manual pouring. By managing these flow characteristics, manufacturers can maintain high speeds without sacrificing the quality or the cleanliness of the production environment.
Dosing Methods Used in Powder Packaging Technology
Different types of powders require specific dosing mechanisms to ensure the weight remains consistent throughout a long production run:
- Auger Fillers for Non Free Flowing Powders: A rotating screw moves specific volumes of powder like flour or ground spices downward with high precision.
- Volumetric Cup Fillers for Uniform Granules: These use pre sized cups to measure out products like sugar or salt that flow easily under gravity.
- Net Weigh Systems for High Value Goods: Every dose is weighed on a precision scale before it is dropped into the package to ensure zero waste.
- Vacuum Filling for Extremely Fine Dust: Pressure differences are used to pull very light powders into the container, minimizing the plume of dust.
- Vibratory Trays for Fragile Granules: Gentle shaking moves the product forward without grinding the particles into a fine dust.
- Timed Flow for Consistent Density: The system opens the filling valve for a specific duration based on a pre calibrated flow rate.
Each of these methods is chosen based on how the specific powder behaves under pressure and movement.
Applications Within the Modern Food Industry
The food sector relies on automated filling to manage everything from bulk ingredients to high end specialty items:
- Spices and Seasoning Blends: Enclosed systems preserve the volatile oils and aromas that give spices their flavor while preventing cross contamination between different batches.
- Bakery Ingredients like Flour and Sugar: High speed lines can fill bags at rates that manual labor cannot match, meeting the needs of large retail chains.
- Instant Beverages and Coffee: Protecting ground coffee from oxygen is vital, and machines can inject nitrogen during the fill to keep the product fresh.
- Nutritional and Protein Powders: Accurate dosing ensures that every scoop provides the exact amount of protein and vitamins listed on the label.
- Dairy Products like Powdered Milk: These systems must meet strict hygiene standards to prevent bacterial growth and ensure a long shelf life.
- Baking Mixes with Multiple Components: Machines can be set to mix and fill various powders in one cycle, ensuring a consistent blend in every box.
These applications show how automation supports the diverse needs of the food supply chain.
Technical Features of Industrial Powder Machinery
To handle the stress of 24/7 production, these machines include several specialized mechanical features:
- Stainless Steel Contact Parts: Usually made from #304 or #316 steel, these parts are easy to sanitize and do not react with food or chemicals.
- Servo Driven Auger Motors: Using servos instead of standard motors allows for much tighter control over the rotations of the filling screw.
- Dust Extraction Ports: These sit near the filling nozzle to suck away stray particles before they can settle on the bag’s seal area.
- Modular Changeover Parts: Different size bags or bottles can be handled by swapping out a few key components in under twenty minutes.
- User Friendly Touchscreen Controls: Operators can store “recipes” for different products, allowing for instant recalibration when switching batches.
- Safety Guarding and Sensors: Integrated shields protect workers from moving parts and stop the machine instantly if a door is opened.
These features ensure that the machinery remains a durable asset in a demanding manufacturing environment.
How Medical Sectors Use a Pharmaceutical Packaging Machine
In the medical industry, the requirement for precision and sterility is even higher than in the food sector, making a pharmaceutical packaging machine a vital component of the facility. These systems are used to fill vials, bottles, or blister packs with active medicinal powders where even a milligram of variation could change the effectiveness of the treatment. These machines are built to operate within clean rooms, featuring specialized air purge systems that ensure no external pollutants enter the filling zone. Because many medical powders are sensitive to static electricity, the equipment includes neutralizing bars that prevent particles from sticking to the container walls or the filling nozzle. Furthermore, these systems are designed for total traceability, printing batch codes and expiration dates directly onto the package while checking the accuracy of every fill. This ensures that if a problem is ever detected, the manufacturer can identify exactly which units are affected. By using this specialized technology, labs and medical companies can guarantee that their products are pure, accurately dosed, and fully compliant with the strict health regulations found in the healthcare market.
Ensuring Airtight Seals to Preserve Freshness
A perfect fill is only effective if the final seal can protect the product from the environment:
- Thermal Heat Sealing: Applying consistent heat to the film creates a bond that moisture and air cannot penetrate.
- Ultrasonic Sealing Options: For heat sensitive powders, sound waves are used to create a seal without affecting the product’s temperature.
- Gas Flushing Integration: Replacing the air inside a bag with nitrogen before sealing helps prevent the oxidation of fats and oils.
- Hermetic Cap Induction: For bottles, an induction sealer bonds a foil liner to the rim, providing a tamper evident and airtight barrier.
- Validation of Seal Strength: Advanced machines can test the integrity of a seal in real time, rejecting any unit that might leak.
- Clean Seal Technology: Vacuum systems ensure that no powder dust is trapped in the seal, which is a common cause of leaks in manual packaging.
A secure seal is the final promise of quality that the manufacturer makes to the end consumer.
The Importance of Hygiene and Sanitization Protocols
Maintaining a clean machine is a daily requirement to prevent cross contamination and ensure food safety:
- Washdown Rated Frames: The entire structure is often built to withstand direct spraying with water and chemical cleaners.
- No Dead Corner Design: Internal parts are rounded and polished so that powder cannot hide in crevices and grow bacteria.
- Tool Less Disassembly: Operators can remove the auger and hopper quickly for a deep clean between different flavors or ingredients.
- Air Purge Systems: Compressed air is used to blow out internal mechanical areas, keeping them free from dust buildup.
- Separation of Mechanical Parts: Motors and gearboxes are physically isolated from the product filling zone to prevent any lubricant leaks.
- Sterile Fill Options: For medical use, the entire filling path can be treated with steam or UV light to ensure total sterility.
Following these protocols ensures that the machinery meets the highest standards of the Unani or modern medical traditions.
Strategic Business Advantages of Automating the Line
Investing in high speed filling technology affects every part of a business, from the warehouse to the accounting department. One of the most obvious gains is the reduction in labor costs, as one person can oversee a machine that does the work of several manual stations. However, the more hidden advantage is the reduction in material waste. Because an automated system is so precise, it avoids the “overfilling” that many companies do to stay safe, which can save thousands of dollars in ingredients over a year. The speed of these systems also allows a brand to be more responsive to market trends; if a certain powder blend goes viral, the production can be ramped up instantly to meet the surge. Furthermore, the professional look of a machine sealed bag or bottle builds more trust with retailers and distributors than a hand sealed alternative. This reliability creates a strong foundation for scaling a business from a local operation to a regional or national presence. By choosing to automate, a company is choosing to move toward a future where efficiency and safety are the top priorities.
Automation is not just about replacing hands; it is about providing those hands with better tools to ensure safety.
Common Misconceptions About Powder Filling Tech
Many business owners hesitate to automate because of myths that no longer apply to modern systems:
- Myth: Machines Are Too Hard to Clean: Modern designs focus on “quick change” and “easy wash” parts that simplify the sanitization process.
- Myth: You Need a Scientist to Run It: Touchscreen interfaces are as simple to use as a smartphone, with pre set recipes for every product.
- Myth: They Only Work for One Type of Bag: Most machines are highly adjustable and can handle various widths, lengths, and styles with simple part swaps.
- Myth: Automated Systems Waste Too Much Film: Precision sensors ensure that film is pulled to the exact length needed, often saving more material than manual methods.
Clearing up these myths helps manufacturers see that automation is a practical and necessary step for growth.
Future Trends in Powder Handling Technology
The packaging industry is moving toward smarter and more sustainable solutions:
- AI Driven Weight Correction: Systems that can automatically adjust the auger speed if they detect a change in the powder’s density.
- Compatibility with Eco Friendly Films: Machines are being updated to run compostable and recyclable materials without slowing down.
- Remote Monitoring via Smartphone: Business owners can check production speeds and error rates from anywhere in the world.
- Reduced Energy Consumption: Newer motors and heaters use less electricity, helping brands meet their sustainability goals.
- Integrated Vision Inspection: Cameras that can spot a tiny wrinkle in a seal at high speeds and reject the bag automatically.
- Modular Expansion Kits: Machines that allow you to add more filling lanes as your business grows, preventing the need for a whole new system.
Staying ahead of these trends ensures that a production facility remains competitive for years to come.
Comparing Powder Filling Equipment Solutions
|
Feature |
Auger Filling Systems |
Volumetric Cup Fillers |
Net Weigh Systems |
|
Best Application |
Fine, non free flowing powders |
Granular, free flowing goods |
High value, precise dosing |
|
Accuracy Level |
High (Volume based) |
Moderate (Size based) |
Extremely High (Weight based) |
|
Speed Range |
20 – 100+ units/min |
30 – 120+ units/min |
10 – 40+ units/min |
|
Dust Control |
Integrated Hoods |
External Required |
Integrated Enclosures |
|
Primary Benefit |
Handling difficult powders |
Fast and cost effective |
Zero product giveaway |
FAQs About Powder Filling and Packaging
How do I stop dust from getting into the bag seal?
Modern machines use dust extraction ports and “staged” filling to keep the seal area clean before the heat bars engage.
Can one machine handle both spices and flour?
Yes, as long as a thorough cleaning is performed between batches to prevent cross contamination and flavor transfer.
What is the benefit of nitrogen flushing for powders?
It removes oxygen from the bag, which prevents rancidity in oils and extends the shelf life of coffee and milk powders.
Are these machines safe for pharmaceutical use?
Specialized versions made from 316 stainless steel are designed specifically to meet the strict sterility and tracking requirements of the medical field.
How long does it take to change from one bag size to another?
With modern quick change parts, a trained operator can typically switch sizes in twenty to thirty minutes.
Wrapping It Up
The transition to automated powder handling is a significant step for any manufacturer in the food or medical sectors. By utilizing a precision powder filling machine, businesses can ensure that their products are accurately measured, securely sealed, and protected from the environment. These systems offer a level of consistency that manual labor simply cannot provide, reducing waste and increasing the speed of the production line. From the initial introduction of the raw material to the final airtight seal, every step is designed to maintain the highest levels of hygiene and safety. Whether you are packaging basic kitchen staples or life saving medicinal compounds, the right technology acts as the foundation of a successful and scalable operation. As consumer demand for transparency and quality continues to grow, having a reliable and efficient packaging line will be the key to staying competitive and building a brand that patients and customers can trust.
The final package is the physical evidence of a manufacturer’s commitment to quality.