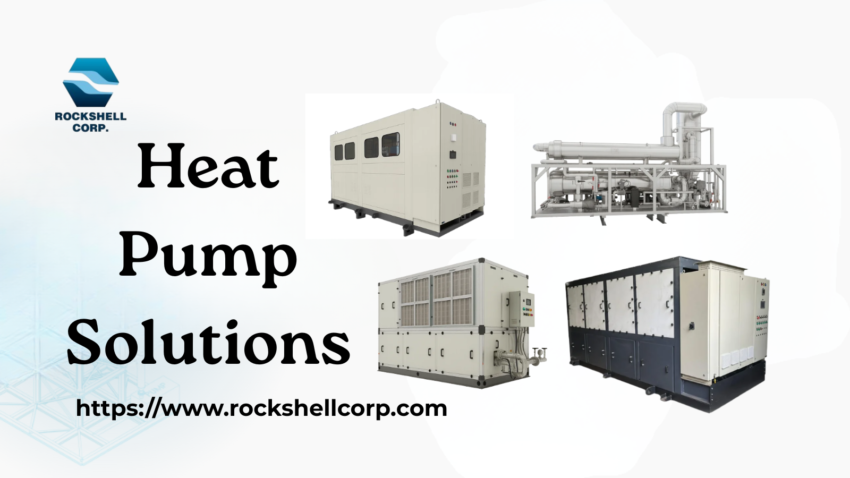
Industries are increasingly adopting the Waste Heat Recovery Heat Pump to improve energy efficiency, reduce operational costs, and support sustainability goals. Among the available refrigerants, ammonia has gained attention because of its excellent thermodynamic properties and high efficiency in industrial applications. However, ammonia-based systems also require strict safety measures due to the refrigerant’s toxicity and flammability characteristics.
When designed and operated correctly, ammonia heat pumps can deliver reliable and safe performance in manufacturing plants, food processing facilities, chemical industries, and other industrial environments. Understanding the key safety considerations is essential for businesses planning to invest in industrial heat recovery systems.
Why Ammonia Is Used in Industrial Heat Pumps
Ammonia is widely used in industrial refrigeration and heat recovery applications because it offers high energy efficiency and excellent heat transfer capabilities. Compared to synthetic refrigerants, ammonia has a lower environmental impact and zero ozone depletion potential.
A modern Waste Heat Recovery Heat Pump using ammonia can efficiently recover low-grade waste heat from industrial processes and convert it into useful thermal energy. This recovered heat can then be reused for steam generation, hot water production, or process heating, helping industries lower fuel consumption and reduce carbon emissions.
Despite these advantages, ammonia requires careful handling because even a small leak can pose health and safety risks. Therefore, industries must focus on system design, monitoring, and operator training.
Proper System Design and Ventilation Are Essential
One of the most important safety measures in ammonia-based heat pump systems is proper equipment design. Industrial facilities should ensure that all pressure vessels, piping, valves, and compressors comply with recognized industrial safety standards.
Additionally, machine rooms must have adequate ventilation systems to prevent ammonia gas accumulation. Proper airflow helps dilute any accidental leakage and reduces the risk of hazardous exposure. Emergency exhaust systems are also critical in enclosed spaces where ammonia equipment is installed.
Industrial heat recovery units should be designed with leak detection systems that provide early warnings. These systems can automatically trigger alarms and ventilation controls if ammonia concentration exceeds safe limits.
Leak Detection and Emergency Response Planning
Because ammonia has a strong odor, small leaks are usually detected quickly. However, relying only on smell is not enough in industrial environments. Facilities should install advanced ammonia gas detectors in high-risk areas such as compressor rooms, pipelines, and storage sections.
A well-planned emergency response strategy is equally important. Every facility using an ammonia-based Waste Heat Recovery Heat Pump should establish procedures for evacuation, leak isolation, and first aid. Emergency shutdown systems must be tested regularly to ensure fast response during critical situations.
In addition, industries should maintain personal protective equipment (PPE) such as gloves, goggles, respirators, and protective clothing for maintenance teams and emergency personnel. Routine safety drills can also improve staff preparedness and minimize risks during unexpected events.
Regular Maintenance and Operator Training Improve Safety
Preventive maintenance plays a major role in ensuring the safe operation of ammonia heat pumps. Over time, components such as seals, valves, and pipelines may wear out, increasing the chances of leakage. Scheduled inspections help identify issues before they become major safety concerns.
Industries should also keep accurate maintenance records and conduct periodic pressure testing. Using high-quality components and certified spare parts further improves system reliability.
Equally important is operator training. Employees handling ammonia-based systems must understand refrigerant behavior, safety procedures, and emergency protocols. Proper training helps operators respond quickly and confidently if abnormal conditions occur.
Modern industrial heat pump manufacturers often integrate automation and remote monitoring technologies that enhance operational safety. These systems can track pressure, temperature, and refrigerant levels in real time, allowing faster corrective action.
Compliance With Industrial Safety Standards
Industrial facilities must comply with local and international safety regulations when installing ammonia heat pumps. Compliance includes proper system labeling, safe refrigerant storage, equipment inspection, and adherence to environmental guidelines.
Working with experienced manufacturers and engineering partners ensures that the system design follows industry best practices. Companies specializing in waste heat recovery technologies often provide customized safety solutions based on the facility’s operational requirements.
Choosing a professionally engineered Waste Heat Recovery Heat Pump not only improves efficiency but also supports long-term operational safety and sustainability.
Conclusion
Ammonia-based heat pumps offer an efficient and environmentally responsible solution for industrial energy recovery. However, safe operation depends on proper system design, ventilation, leak detection, preventive maintenance, and employee training.
When industries invest in a well-designed Waste Heat Recovery Heat Pump, they can achieve significant energy savings while maintaining high safety standards. Partnering with experienced industrial heat recovery solution providers can help businesses implement reliable and compliant systems tailored to their operational needs.
As industries continue to focus on energy efficiency and carbon reduction, ammonia-based heat recovery systems are expected to play an increasingly important role in sustainable manufacturing.